Technical Article
CNC Ceramic Machining: From Design Files to Custom Precision Components
CNC makes custom ceramic components possible by controlling the motion of tools that shape a ceramic blank or finish its functional surfaces. The right operation depends on the material and its manufacturing stage: green or partially fired bodies can be cut before final sintering, dense technical ceramics usually require diamond-abrasive machining, and specially machinable grades can accept conventional cutting tools. CNC provides repeatable motion; the material, tooling and process plan determine whether that motion produces a reliable part.
For product customization, the main benefit is translating a specific design into controlled features: an insulating block's mounting pattern, a ring's locating diameter, a nozzle's bore or a plate's mating surface. CNC can support prototypes and small batches without a dedicated forming tool for every shape. It also remains useful in volume production when selected dimensions need finishing after firing. Its value is therefore broader than making complex shapes: it connects design changes, material behavior, assembly requirements and inspection.
What CNC actually controls in ceramic machining
Computer numerical control coordinates a machine's axes, tool movements and programmed operations. It can guide milling, turning, drilling and grinding equipment, including specialized machines for hard and brittle materials. CAD describes the part; CAM helps create the toolpath; the machine executes a verified program with the selected tools, fixtures and process conditions.
The word CNC does not identify the removal mechanism. A cutting edge milling a binder-containing compact behaves differently from a diamond grinding pin working on fired alumina. Likewise, machining with a ceramic cutting insert usually means using that insert to cut another material; it does not necessarily mean machining a ceramic workpiece. Buyers should ask which ceramic grade, material state and operation a supplier is proposing.
A useful quotation consequently describes the route rather than simply saying that a part is CNC-machined. It identifies what is formed, what is cut before firing, which surfaces are finished after firing and how the finished requirements will be measured. This makes competing quotations easier to compare and exposes features that need an early design discussion.
Three material states require different strategies
Green and partially fired ceramics
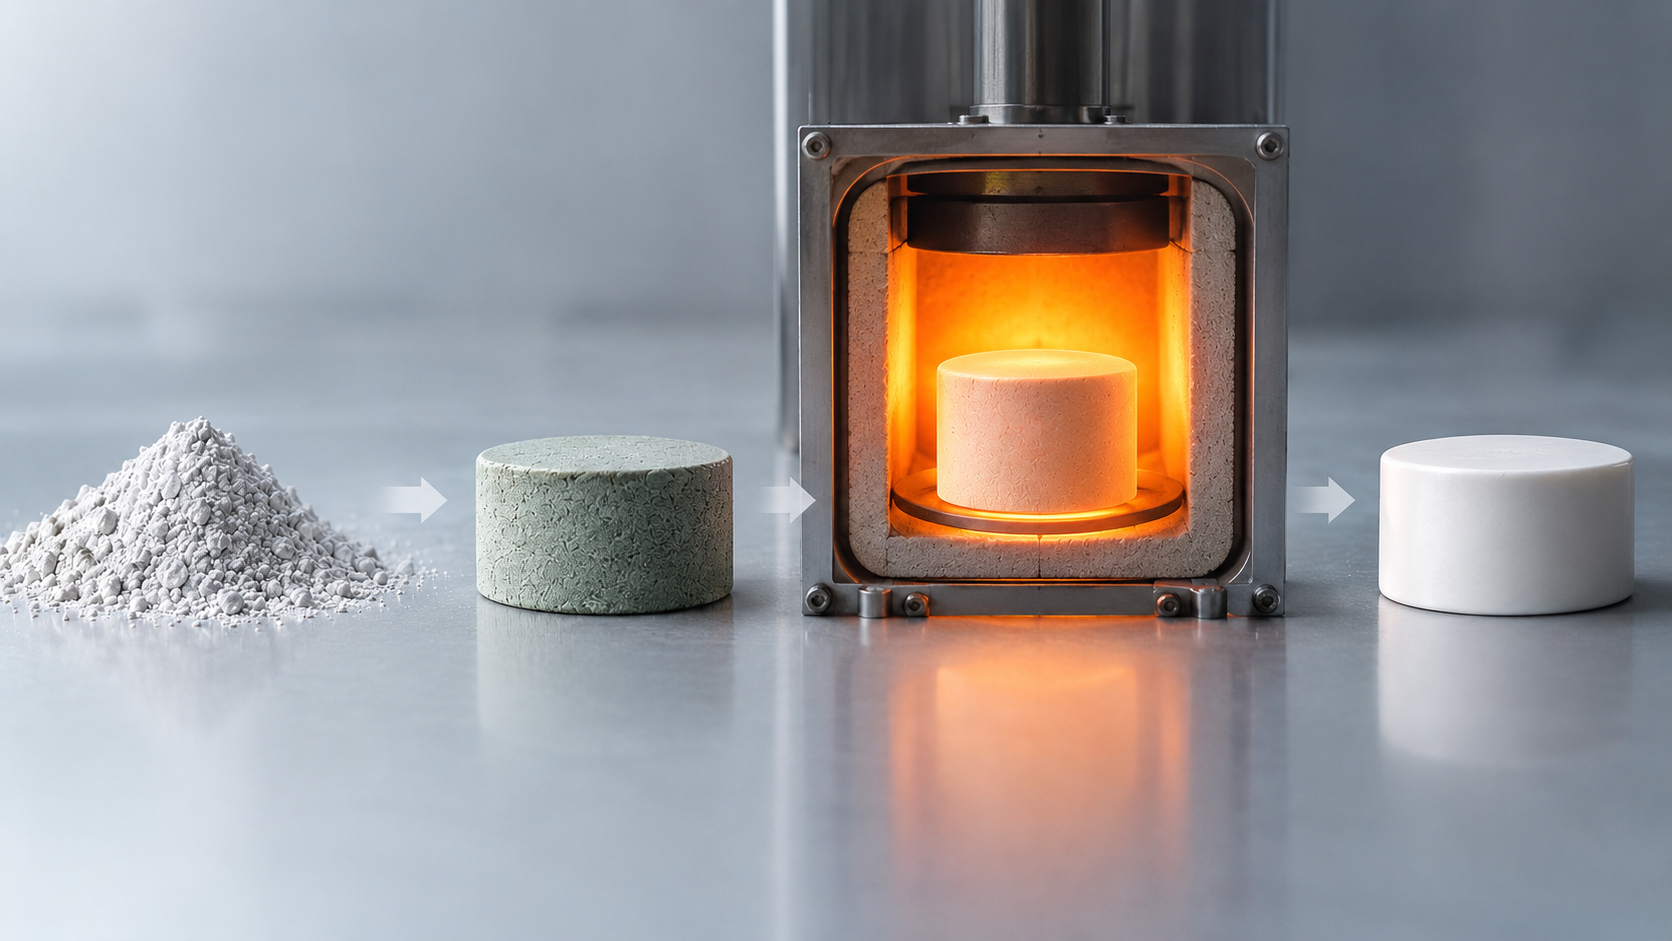
Green machining shapes a formed ceramic body before full densification. The body can still contain temporary processing additives. A partially fired, sometimes called white or biscuit, body offers another intermediate state. Terminology and the degree of pre-firing vary, so the supplier should identify the condition actually being machined.
These stages can be economical for removing substantial material and producing features that are difficult to obtain directly from a forming tool. However, the workpiece remains vulnerable to handling and machining damage, and subsequent firing still changes its dimensions. The European Commission's ceramic-manufacturing draft reference document distinguishes green, white and hard machining by their place in the manufacturing sequence. [1]
Fully sintered technical ceramics
Once a dense ceramic has reached its final fired state, its hardness and brittle response change the machining problem. Diamond-abrasive grinding, cutting and drilling are common routes for dense alumina, zirconia, silicon nitride and silicon carbide. The exact operation depends on the grade and feature; a conventional metal-cutting program cannot simply be transferred unchanged.
Post-sinter machining works on the part after its major firing-related dimensional changes. That makes it valuable for establishing final fits, datum relationships and functional surfaces. It also concentrates effort in a material that is expensive to remove. The manufacturing plan should justify which surfaces need this control rather than assigning precision finishing to every face.
Specially machinable grades
Some glass-ceramics and certain boron-nitride-containing or other specially formulated materials are designed for easier machining. Conventional tooling can be practical within a grade's documented guidance. Their behavior should not be generalized to all ceramics, and their service properties must still satisfy the application.
An easily machined substitute may make a prototype convenient, but does not automatically reproduce the strength, thermal behavior, electrical characteristics or chemical resistance of the intended production ceramic. A dimensional mock-up and a functional qualification part serve different purposes. Define which type of prototype is needed before choosing the blank.
| Workpiece condition | Typical machining approach | Contribution to customization | What must be confirmed |
|---|---|---|---|
| Green body | CNC cutting, turning, drilling or profiling suited to the compact | Generates custom geometry before the body becomes hard | Handling strength, support, remaining shrinkage and firing behavior |
| Partially fired body | Grade-specific cutting or abrasive operations | Offers an intermediate route for features difficult in the green state | Actual pre-firing condition and remaining dimensional change |
| Fully sintered dense ceramic | CNC diamond grinding, abrasive drilling, cutting and finishing | Establishes final interfaces and dimensional relationships | Tool access, stock, edge integrity and inspection |
| Specially machinable ceramic | Conventional or diamond tooling according to grade guidance | Supports flexible machining from suitable stock shapes | Material suitability, tooling guidance and finished-part requirements |
How a custom drawing becomes a manufacturable component
Establish the function before generating toolpaths
A custom ceramic project should begin with what the part must do. Electrical insulation, wear resistance, dimensional stability, thermal transfer and chemical compatibility lead to different material choices. The drawing then defines the surfaces and relationships that deliver that function. A CAD shape alone does not explain whether a pocket is cosmetic, a locating feature or a cleanable process passage.
The engineer and manufacturer should identify mating parts, assembly loads, operating conditions and the reason for each critical tolerance. This discussion can reveal that a generous clearance is acceptable in one area while another interface needs controlled flatness or position. CNC programming becomes more effective when these priorities are settled before material is removed.
Select a blank and allocate the operations
The starting point might be a pressed compact, an extruded shape, a molded preform or a fired stock blank. Availability, grade, size and quantity influence the route. A prototype can sometimes be made from stock while the production version uses a near-net forming process followed by limited machining.
The manufacturer assigns operations to the stage where they are practical and economical. Large recesses may be created before firing; final locating surfaces may be finished afterward. Our separate discussion of green machining and diamond grinding explains this stage-selection decision in more detail. The customization task is to connect that choice to the actual assembly and inspection needs.
Plan shrinkage and finishing allowance
When machining takes place before full sintering, dimensions must anticipate the remaining densification. A simple scale factor can illustrate the idea, but a production compensation model must reflect the material, forming route, direction and process history. Local distortion cannot necessarily be corrected by enlarging every CAD dimension equally.
Finishing stock also needs deliberate allocation. Too little can leave a fired surface that cannot clean up; too much adds grinding time and risk. The supplier should specify the allowance and how the blank will be supported through firing. Buyers should avoid imposing a universal shrinkage percentage or stock allowance without evidence for the specific process.
Program the sequence around datums and access
A CAM strategy must account for tool shape, reach, fixture clearance and the order in which support material disappears. Several setups can be necessary. The datum used to locate an early blank may not be the final assembly datum, so the plan must explain how important relationships are established after the part changes state or is repositioned.
Multi-axis CNC can improve access and reduce some repositioning, but it does not make every internal corner or passage reachable. A tool still has a diameter, a working length and a stiffness limit. Some designs need a different forming route, a separate insert, a joined assembly or a revised feature rather than a more elaborate toolpath.
Why ceramic machining needs different process control
Control damage as well as dimensions
Ceramics often fail through flaws rather than visible plastic deformation. Grinding can create surface or subsurface cracks, and the appearance of a smooth face does not establish the condition beneath it. NIST's fractography guide explains how successive grinding and polishing steps can control damage left by earlier operations, while also highlighting the susceptibility of edges to chipping. [2]
This is why aggressive roughing followed by a cosmetic polish is not automatically a sound process. Tool condition, removal strategy and the finishing sequence must work together. Small edge treatments can help handling and assembly, but their geometry and acceptance limits should be specified instead of being left to an ambiguous instruction to break all edges.
Support the workpiece without overloading it
Fixtures must locate the component and resist machining forces without introducing damaging concentrated loads. Broad support, controlled contact and an appropriate sequence are especially important for thin sections and fragile intermediate bodies. The fixture used for a robust metal part may be unsuitable for an otherwise similar ceramic shape.
Workholding also influences dimensional results. A part distorted while clamped may appear acceptable in the machine and change shape when released. Define how it is supported during inspection as well as machining. Where a thin plate's free-state condition matters, that requirement should be understood before the shop chooses its fixture.
Manage tools, fluid and debris as a system
Diamond tool selection includes more than the presence of diamond. Abrasive size, bond, geometry, wear and conditioning affect the operation. Coolant delivery and debris removal must be suited to the tool, grade and cleanliness requirements. No single speed, feed or fluid recommendation is appropriate for every ceramic.
The manufacturing plan should include contamination control and cleaning after machining. Fine abrasive debris left in a bore or channel can matter in a precision assembly. Machine protection and suitable containment are also necessary because ceramic debris is abrasive; these are process-engineering decisions rather than reasons to assume any ordinary CNC installation is ready for ceramics.
What CNC contributes to product customization
Prototype flexibility and controlled design changes
A programmed route can make a new pattern, pocket or profile without a new dedicated mold for each iteration, provided that a suitable blank and machining access exist. This helps engineers test fit and function before committing to a higher-volume route. Programming, fixtures and inspection still require preparation, so flexible does not mean instantaneous or tooling-free.
Changes should be tied to a drawing revision. A revised bore, edge relief or locating feature may affect more than one operation. Version control connects the CAD file, program, setup sheet and inspection plan, reducing the risk that the geometry is updated while an old acceptance requirement remains in use.
Functional interfaces that fit the actual assembly
CNC finishing can establish a component's final locating diameter, mating face, precision bore or controlled thickness. The important result is the relationship between features, not simply the number of axes on the machine. A ring can meet its diameter tolerance yet still fail assembly if its locating face and bore are not related correctly.
This is particularly valuable when the ceramic must interface with metal, another ceramic or a precision fixture. Thermal expansion, contact stress and assembly method should be considered alongside the room-temperature drawing. A well-finished part is useful only when the selected interfaces suit its working environment.
A bridge from trial parts to repeatable supply
The prototype route can provide information about achievable geometry, finishing effort, inspection access and likely yield risks. It does not automatically become the lowest-cost production route. As quantity rises, pressing, molding or another near-net process may remove more work before CNC finishing begins.
CNC can then concentrate on the features that forming and firing do not consistently deliver to the required final state. Its role changes from generating much of the part to controlling a smaller group of interfaces. The program, fixture and inspection plan should be requalified when the starting blank or forming route changes.
| Customization need | How CNC can help | Boundary to discuss early |
|---|---|---|
| New prototype geometry | Adapts a program to an available blank or preform | Material availability, setup effort and machining access |
| Small-batch variants | Changes selected holes, profiles or interfaces | Revision control and repeatable locating strategy |
| Tight assembly relationships | Finishes datums and related features after firing | Full tolerance stack and inspection method |
| Seal or wear surface | Supports controlled grinding and subsequent finishing | Form, texture, edge condition and surface integrity |
| Transfer to production | Retains selective finishing while forming supplies near-net geometry | New blank behavior and process requalification |
An illustrative custom insulating block
Consider a ceramic insulating block with a deep clearance pocket, mounting holes and a locating face. This is an engineering example, not a report of a tested customer product. The first review identifies which features provide electrical clearance, which locate the block and where assembly contact loads occur.
The pocket may be economical to machine before firing if its geometry and final variation are acceptable. Mounting holes might be created early with clearance sufficient for the assembly, or reserved for a later operation if their final position is critical. The locating face can be finished after firing when it establishes the component's final relationship to the equipment.
Inspection then follows those functions: the pocket must provide clearance, the hole pattern must assemble and the locating face must satisfy its form and position requirements. This example shows what CNC customization actually delivers: a controlled route from a functional drawing to a part that can be evaluated against explicit acceptance criteria.
Inspection determines whether customization has succeeded
A machine's positioning specification is not the tolerance of a finished ceramic part. The result also includes tool wear, fixturing, temperature, material variation, firing history and measurement uncertainty. Quoting a nominal machine accuracy as a blanket part capability leaves out much of the process.
Agree on datum references and measurement methods before manufacturing. Size, flatness, position and roughness describe different properties. A low roughness value does not prove flatness, and a dimensional report does not by itself establish the absence of strength-limiting flaws. NIST's silicon-nitride case study illustrates that grinding direction and wheel grit can affect machining flaws; its results are not a universal strength reduction for every ceramic. [3]
A first-article review should connect the drawing to actual measurements and any required functional tests. For repeat orders, identify the controls that will maintain the result: approved material, blank condition, program revision, tool management, fixture, finishing sequence and acceptance plan. Any strength or reliability claim needs evidence appropriate to the component and application.
What to send for a custom ceramic machining inquiry
Provide a dimensioned drawing and a three-dimensional model, with units, revision and material grade or material-selection requirements. Identify assembly datums, critical fits, functional surfaces and permissible edge conditions. Include quantity, expected repeat volume, operating environment and any cleanliness or traceability requirements.
Ask the manufacturer to explain the proposed forming and machining route, which features are finished after firing, and how acceptance will be demonstrated. Discuss alternatives when a feature is inaccessible or disproportionately expensive. The most useful proposal is not the one that promises every tolerance immediately, but the one that connects your component's function to a feasible and verifiable manufacturing plan.
Frequently asked questions
Have a drawing for a custom ceramic component?
Contact Our TeamEngineering references
- European Commission JRC: ceramic manufacturing draft reference document, green, white and hard machining. Draft published in 2025; process background, not a final standard.
- NIST Recommended Practice Guide: Fractography of Ceramics and Glasses, second edition, section on grinding and machining cracks.
- NIST: On the Fractographic Analysis of Machining Cracks in Ground Ceramics, a Case Study on Silicon Nitride.